7 Ways to Improve Cold Chain Logistics Efficiency
Table of Contents
- 1. Deploy Real-Time Temperature Monitoring with IoT Sensors
- 2. Cold Chain Temperature Monitoring Best Practices for Every Shipment
- 3. Choose the Right Thermal Packaging and Insulation Materials
- 4. Optimize Routes and Lane Mapping with Telematics
- 5. Invest in Cold Storage Facility Management and Automated Handling
- 6. Reduce Human Error Through Training and Sanitation Protocols
- 7. Improve Cold Chain Logistics for Last-Mile Delivery and Sustainability
- The Link Between Cold Chain Logistics and Long Term Stability of Lyophilized Peptides
- Frequently Asked Questions
Last Updated: October 2, 2026
1. Deploy Real-Time Temperature Monitoring with IoT Sensors
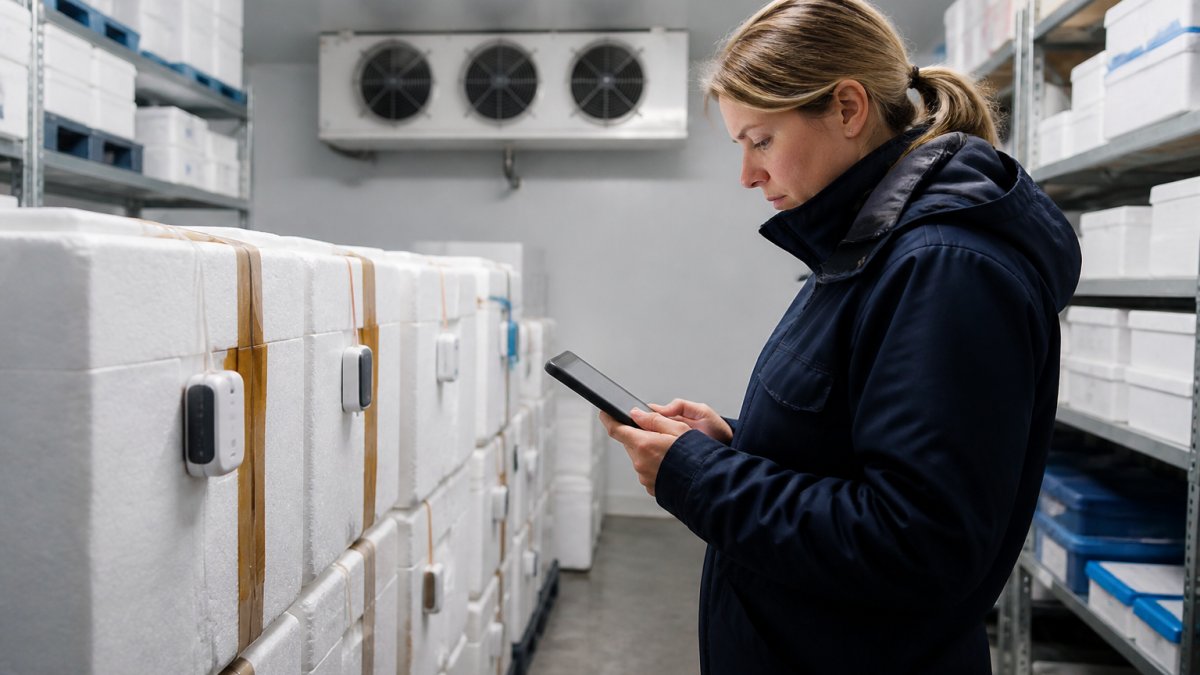
A cold chain breaks most often in the gap between what a data logger records and what a dispatcher actually sees. Real-time monitoring closes that gap. IoT sensors stream temperature, humidity, and location data continuously, so a shipment drifting out of range triggers an alert while there is still time to act.
The practical value is in the alert, not the log. A logger tells you a pallet spoiled. A sensor tells you it is spoiling right now, on this truck, at this mile marker.
The Three Layers of a Working Monitoring Stack
Most deployments fail because they buy one layer and assume it covers the other two. A functional system has three:
- Sensing layer. Thermistors and thermocouples are the workhorses for probe-based readings; digital sensors with onboard memory handle pallet-level logging. For single-use shipments, disposable USB and NFC loggers are common because they avoid reverse logistics. For high-value or reusable lanes, cellular and Bluetooth Low Energy (BLE) trackers report in transit rather than on arrival.
- Transmission layer. Cellular (LTE-M and NB-IoT) works where coverage exists and needs no gateway. BLE and LoRaWAN need a gateway or reader at handoff points, which lowers hardware cost but creates blind spots between checkpoints. Satellite backhaul is the fallback for remote lanes where cellular drops out.
- Platform layer. This is where alerts, dashboards, and audit trails live. The platform is what turns raw readings into a decision.
How Automated Alerts Prevent Temperature Excursions
Automated alerts catch excursions at the moment they start, not at delivery. Set thresholds per product, not per trailer.
Alert logic should distinguish three states: in-range, approaching limit, and out-of-range. The middle state is the one that saves shipments.
Platforms like Tive handle this with cellular-connected trackers that report temperature and location end to end. The tradeoff is real: every shipment needs hardware, and hardware needs recovery.
Set your alert thresholds 2°C inside the actual product limit. That buffer gives your team time to respond before the shipment crosses the line that matters.
Validation and Calibration Are Not Optional
An uncalibrated sensor produces confident, wrong data. Under current good manufacturing practice expectations, monitoring instruments used for product-release decisions need documented calibration against a traceable reference, and the calibration interval should match the sensor’s drift characteristics, not a calendar default. Keep the certificate with the shipment record so a receiving lab or auditor can reconcile the reading to the instrument that produced it.
What to Measure Beyond Temperature
Temperature alone misses failure modes that matter. Humidity swings drive condensation and can compromise packaging and product alike. Door-open events and shock/vibration readings explain why an excursion happened, which is what turns a monitoring system into a continuous-improvement tool rather than a claims file. Light exposure matters for some pharmaceutical and biological shipments. The more of these a single tracker captures, the fewer separate devices you have to manage.
2. Cold Chain Temperature Monitoring Best Practices for Every Shipment
Cold chain temperature monitoring best practices come down to three things: calibrate the sensors, document the range for each product, and keep an unbroken record from dock to dock. A monitoring system is only as good as the calibration behind it. Uncalibrated sensors produce confident, wrong data.
Build a simple shipment profile before anything leaves the dock:
- Confirm the required temperature range for each product in the load
- Verify sensor calibration date and certificate
- Place sensors at the warmest and coldest points, not just the center
- Record the pre-cooling step and the trailer’s starting temperature
- Assign one person to own the alert response
That last item is where most operations fail. An alert with no owner is just a notification.
3. Choose the Right Thermal Packaging and Insulation Materials
Thermal packaging decides how much time a shipment has before ambient conditions win. Insulation buys hours; the right insulation buys enough hours to reach the destination without a temperature excursion. Match the packaging to the lane, the season, and the duration, not to last year’s default.
| Packaging Type | Best For | Typical Duration | Watch For |
|---|---|---|---|
| Gel packs | Short-haul, refrigerated range | 24-48 hours | Freezing product on contact |
| Dry ice | Frozen range, longer transit | 48-96 hours | Ventilation requirements |
| Thermal pouches | Small parcels, last-mile | 12-24 hours | Gasket wear over time |
| Insulated pallet shippers | Bulk pharmaceutical logistics | 48-120 hours | Pallet handling damage |
| Vacuum insulated panels (VIPs) | Space-constrained, long-duration | 96+ hours | Cost and panel damage |
Dry Ice vs. Gel Packs: Matching the Solution to the Shipment
Dry ice suits frozen shipments that need sustained sub-zero temperatures over multiple days. Gel packs suit refrigerated shipments where a milder, more stable range is the goal. The mistake is treating them as interchangeable. Dry ice sublimates and needs ventilation; gel packs freeze and can damage product that sits against them. Gasket inspection matters for both, because a worn seal undoes good insulation.
Phase Change Materials Change the Math
Phase change materials (PCMs) are the middle path most guides skip. A PCM is engineered to hold a specific temperature, commonly 2°C to 8°C for refrigerated pharma, or around -20°C for frozen, by absorbing or releasing latent heat as it changes phase. Unlike gel packs, a correctly specified PCM holds a narrow band rather than drifting toward freezing or warming toward ambient.
Qualify Packaging, Don’t Assume It
A shipper that performed in January may fail in July. The disciplined approach is a thermal qualification: pack a representative payload with a temperature logger, run it through the actual lane or a chamber that simulates the lane’s ambient profile, and confirm the payload stays in range for the full transit plus a safety margin. Re-qualify when the lane, season, payload mass, or shipper design changes.
The Sustainability Angle Competitors Miss
Packaging is where cold chain sustainability is most winnable. Reusable insulated shippers and PCM panels replace single-use foam and gel, cutting landfill waste and the carbon embedded in disposable materials. Right-sizing the shipper to the payload reduces both material and the refrigerated volume that has to be held, an over-insulated parcel wastes material, while an under-insulated one wastes product. For lanes with consistent volume, a reusable shipper program with a return loop often pays back faster than the per-shipment cost suggests, because the conditioning and cleaning steps are cheaper than buying new disposables every time.
Never swap a packaging component, a thinner panel, a different PCM, a cheaper gasket, without re-qualifying the shipper. A single substitution can silently cut the safe transit window by hours.
4. Optimize Routes and Lane Mapping with Telematics
Route and lane decisions determine how long cargo sits in uncontrolled conditions. Telematics turns that from a guess into a measurement.
Route optimization software handles the sequencing side, prioritizing multi-stop deliveries so perishable goods move first. What it does not do is monitor cargo temperature, so pair it with a monitoring layer rather than treating it as a complete solution.
Skipping preventive reefer maintenance to save on service costs is the most expensive false economy in cold chain logistics. One mid-route compressor failure can destroy an entire trailer load.
5. Invest in Cold Storage Facility Management and Automated Handling
Warehouse handling is where cold chain integrity quietly erodes. Every manual pick, every open door, every minute a pallet sits on a warm dock adds up.
The honest limitation is capital. These systems carry a high upfront cost, and they only pay off at volume. For a smaller operation, the better first move is process discipline: consolidate picks, stage pre-cooled, and keep dock doors closed between transfers.
6. Reduce Human Error Through Training and Sanitation Protocols
Most cold chain failures trace back to a person, not a machine. A door left open, a sensor not reset, a load staged in the wrong zone.
What most guides miss is that training fails when it is a one-time event. Build short, recurring refreshers tied to actual incidents.
Sanitation protocols belong in the same conversation. A clean, dry, well-organized cold storage area is easier to inspect, and inspection is how you catch a failing gasket or a mislabeled pallet before it becomes a loss.
7. Improve Cold Chain Logistics for Last-Mile Delivery and Sustainability
Last-mile is the weakest link in most cold chains. It is the longest uncontrolled stretch, the most variable, and the hardest to monitor.
Two improvements pay off together. First, route density: fewer, fuller vehicles mean less fuel and less time out of temperature control. Second, right-sized packaging: over-insulated parcels waste material, while under-insulated ones waste product.
For temperature-sensitive research materials, this is where supplier practice matters.
The Link Between Cold Chain Logistics and Long Term Stability of Lyophilized Peptides
Cold chain logistics directly determines the long term stability of lyophilized peptides. A lyophilized compound is stable by design, but that stability assumes the cold chain held.
This is why batch-level traceability matters as much as the temperature record.
For researchers running molecular analysis or clinical-grade experiments, the practical takeaway is to treat cold chain documentation as part of the material’s specification, not as paperwork.
Frequently Asked Questions
What are the primary challenges in maintaining cold chain integrity for lyophilized peptides?
Lyophilized peptides are sensitive to temperature fluctuations, humidity, and physical shock. Temperature excursions during transport can cause aggregation or degradation, reducing purity and activity. Other challenges include inadequate thermal packaging, delayed shipments, and lack of real-time visibility. Implementing IoT sensors, using validated thermal pouches or dry ice, and following cold chain temperature monitoring best practices help prevent these issues. Batch-level traceability and Certificate of Analysis documentation also support quality assurance.
How does real-time temperature monitoring improve cold chain logistics?
Real-time monitoring with IoT sensors provides continuous data on temperature and humidity, allowing immediate detection of excursions. Automated alerts enable rapid corrective actions, such as rerouting or replacing compromised coolant, before the entire shipment is lost. This data also supports regulatory compliance and insurance claims. For research materials like peptides, real-time monitoring ensures that the long term stability of lyophilized peptides is maintained, preserving experimental integrity.
What regulatory standards govern the transport of sensitive laboratory materials?
In the United States, the transport of sensitive laboratory materials is governed by agencies such as the FDA (Food and Drug Administration) for pharmaceuticals and biologics, the DOT (Department of Transportation) for hazardous materials, and the USDA for certain biological products. Key standards include Good Distribution Practice (GDP) guidelines, which require documented temperature control and traceability. Compliance ensures product safety and efficacy, and is critical for research-grade materials like peptides and coenzymes.
How can batch-level traceability reduce risks in the cold chain?
Batch-level traceability allows you to track each lot of material from origin to destination, including temperature history and handling. If a deviation occurs, you can quickly identify affected batches and isolate them, preventing compromised materials from reaching experiments. This reduces waste and ensures only validated compounds are used. For lyophilized peptides, traceability combined with multi-stage HPLC testing and mass spectrometry verification provides a complete quality record.
What is the impact of temperature excursions on the long-term stability of coenzymes?
Coenzymes, like peptides, are susceptible to degradation when exposed to elevated temperatures. Even brief excursions can cause hydrolysis, oxidation, or aggregation, leading to loss of enzymatic activity. For long-term stability, lyophilized coenzymes should be stored at -20°C or below and shipped with adequate dry ice or gel packs. Real-time monitoring and validated thermal packaging are essential to maintain integrity throughout the cold chain.
Cold chain failures are expensive, and they are almost always preventable with better monitoring, better packaging, and better documentation. FROPeptides supplies high-purity research peptides and lyophilized coenzymes with temperature-controlled storage, multi-stage HPLC testing, and mass spectrometry verification on every batch, backed by batch-level Certificates of Analysis. Get started with FROPeptides and source research-grade materials you can trace from dispatch to bench.